Flat head (Flat Head)
The simplest and cheapest head, but the weakest against internal pressure
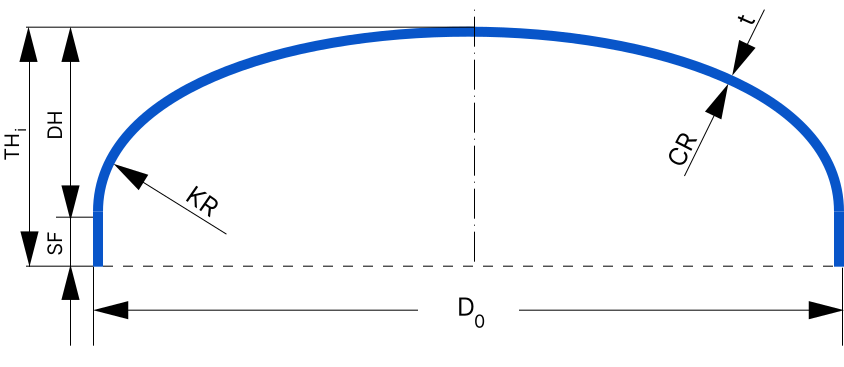
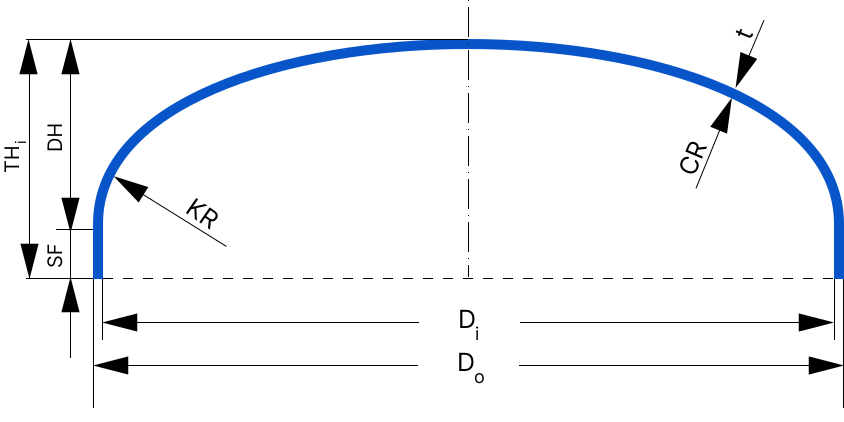
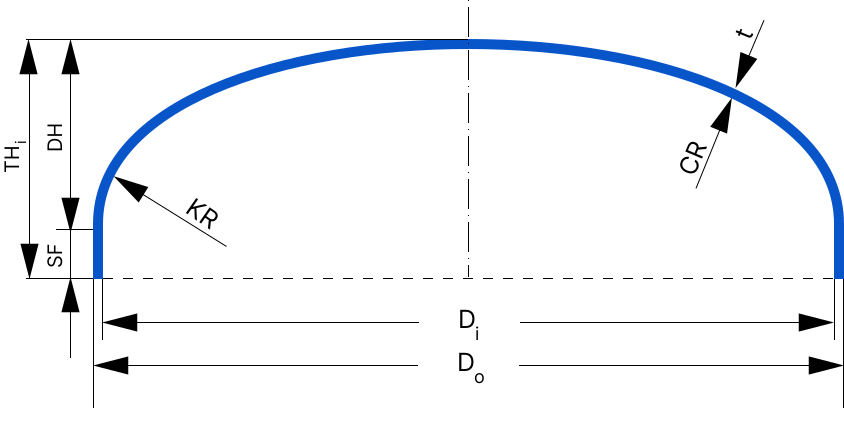
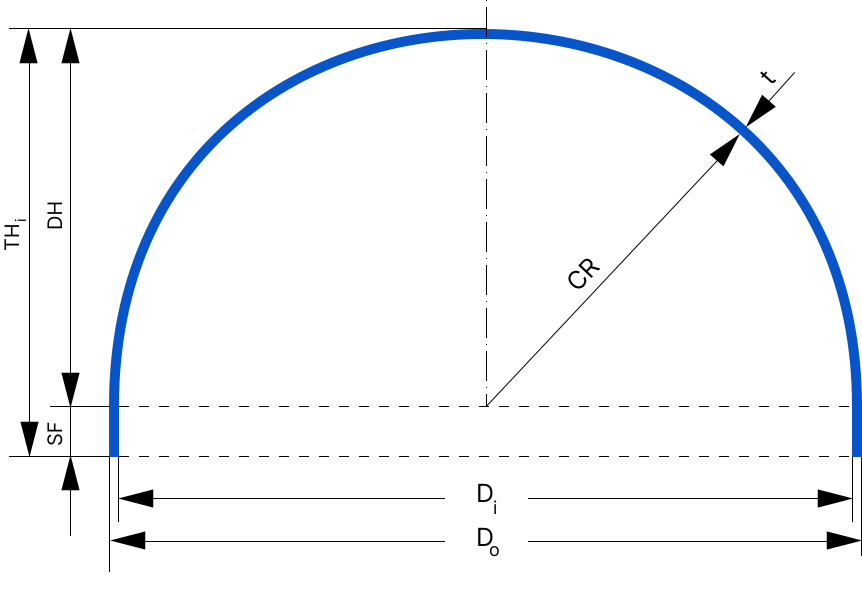
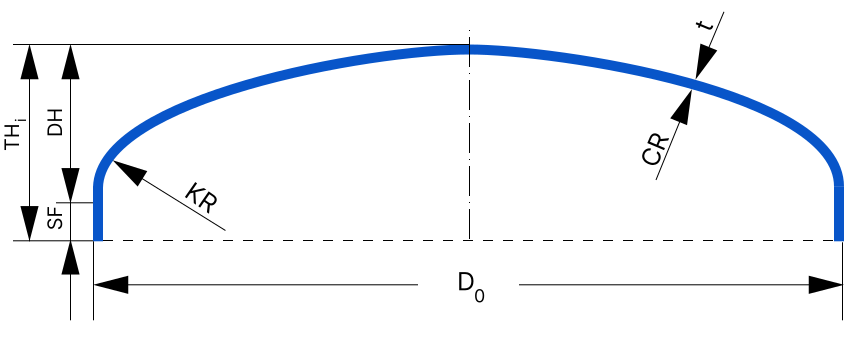
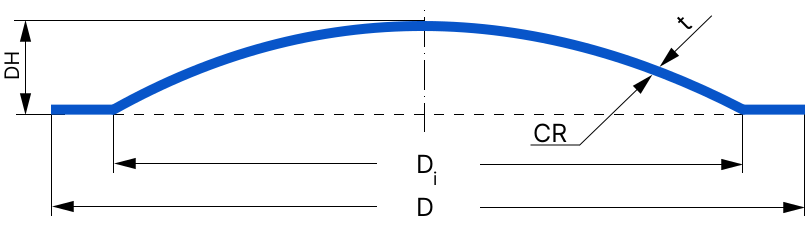
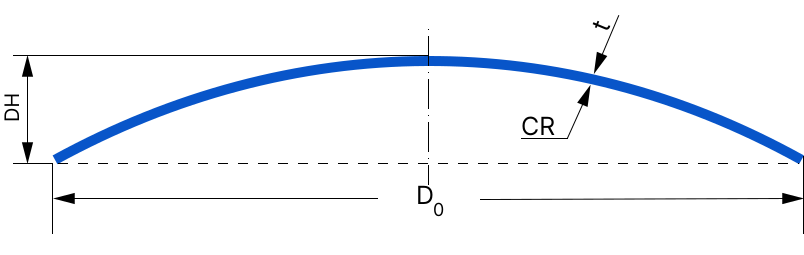
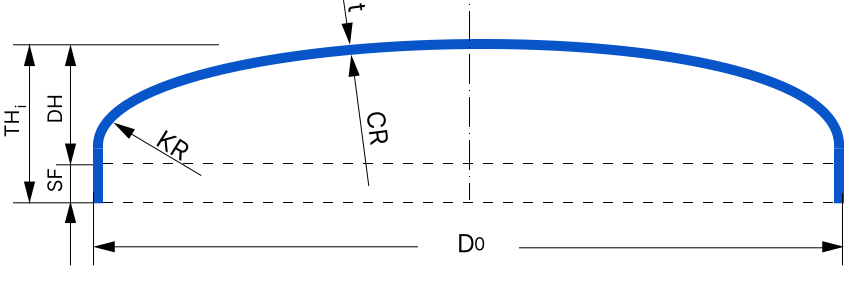
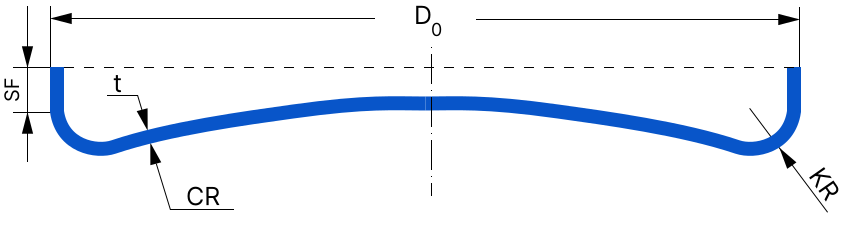
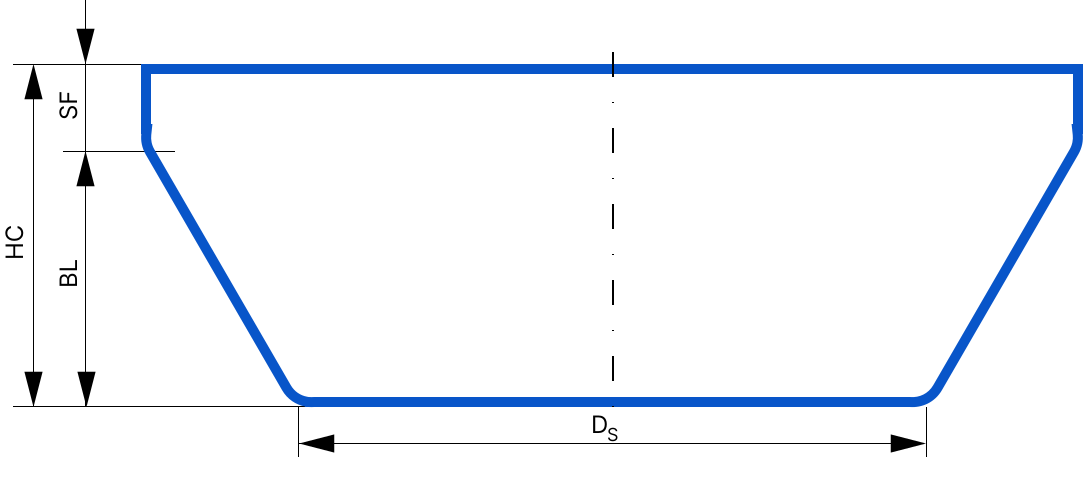
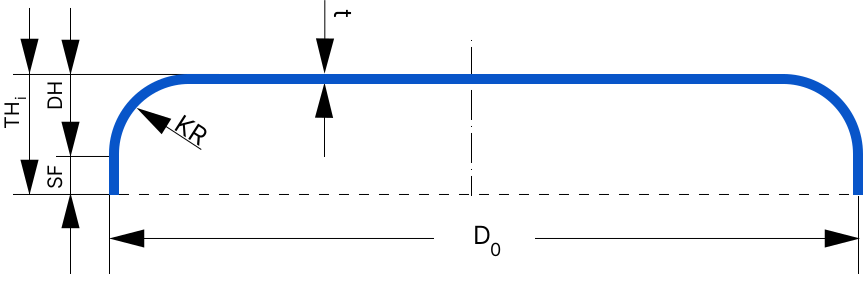
Unlike other types, a flat head has no spherical or elliptical dome; only a small turned-up edge (KR) is formed around it to join the body. The head depth (DH) in this type is exactly this KR, which is taken as at least 0.06×Di or 25 millimetres (whichever is greater).
What is a flat head?
Unlike other types, a flat head has no spherical or elliptical dome; only a small turned-up edge (KR) is formed around it to join the shell. The head depth is exactly this KR.
Because a flat surface tends to bend under pressure perpendicular to it, the thickness needed for a given pressure is far greater than for a formed head of the same diameter; so it only stays economical for small diameters or very low pressure.
Geometry formulas of the flat head
The only main geometric parameter is the radius of the turned-up edge:
In a flat plate under pressure, bending stress rises quickly and there is no curvature to turn the load into membrane stress; for the same pressure, the thickness needed can be several times that of a formed head.
Online calculation
See the head's dimensions, volume and weight for a real diameter and thickness
Flat head (Flat Head)
Liquid level and volume inside this head
How the head is mounted
Development of this head (flat blank before forming)
The diameter of a flat plate of the same thickness and material that weighs the same as the formed head — an initial workshop estimate based on equal weight, not allowing for thickening or extra stretching at the knuckle.
The vessel head production process
From calculating the blank diameter to final edge preparation — the steps of making a vessel head in the workshop
Calculating the blank diameter
Cutting a disc from plate with the diameter and thickness calculated for the head type and vessel diameter
Cutting the plate blank
Precise cutting of steel or stainless plate by plasma, laser or gas according to the technical drawing
Pressing the head
Hot or cold forming of the disc with a die and industrial press until it reaches the final head profile
Edge preparation
Machining the edge, bevelling and preparing the weld area for fitting to the vessel shell
 Video coming soon
Choosing a head: the balance between pressure, cost and time
In a flat plate under perpendicular pressure, bending stress rises rapidly from the centre to the edge, and unlike formed heads there is no curvature to turn part of this load into membrane tensile stress. The result is that for the same design pressure, the thickness a flat head needs can be several times that of an elliptical or torispherical head of the same diameter.
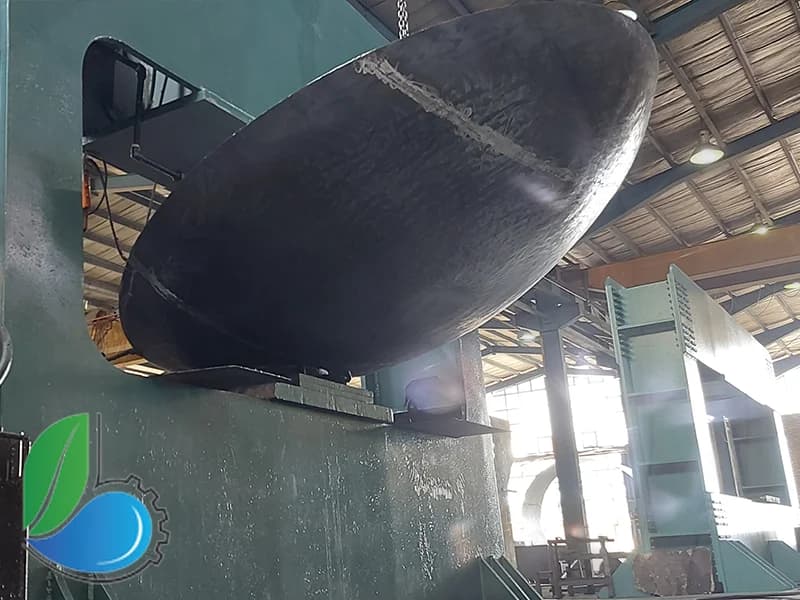
Gallery of heads we have made
Flat head gallery
Applications and industries served


Buying heads from Behineh Ab
Six steps from first contact to delivery
Give the outside diameter, plate thickness, head type and required material.
The calculated weight, unit price and delivery time are sent the same business day.
Plate is supplied with the mill certificate and inspected on arrival before cutting.
Cutting the disc, hot or cold pressing depending on thickness, and checking dimensions with a template.
Machining the cylindrical edge and bevelling it ready for welding to the shell.
Packing, issuing the part identification sheet and shipping nationwide.
What sets us apart
Price inquiry
vessel head
Enter the diameter, thickness and head type; you will receive the calculated weight and unit price.
- Quotation with the exact weight of the part
- Standard heads delivered in 7 business days
- Shipping nationwide