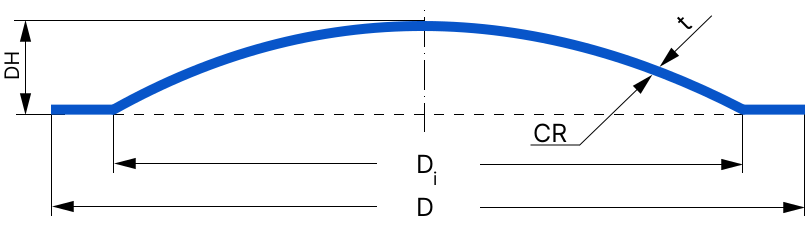
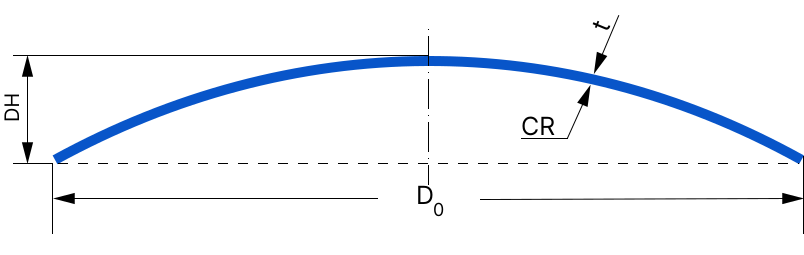
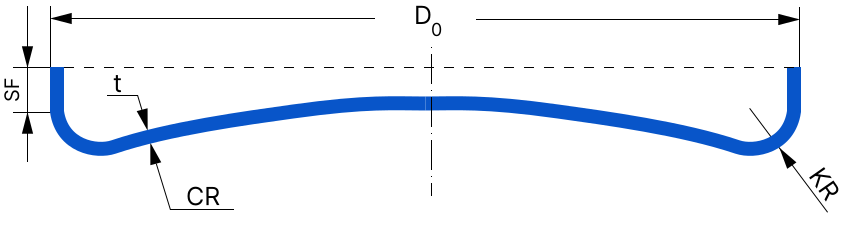
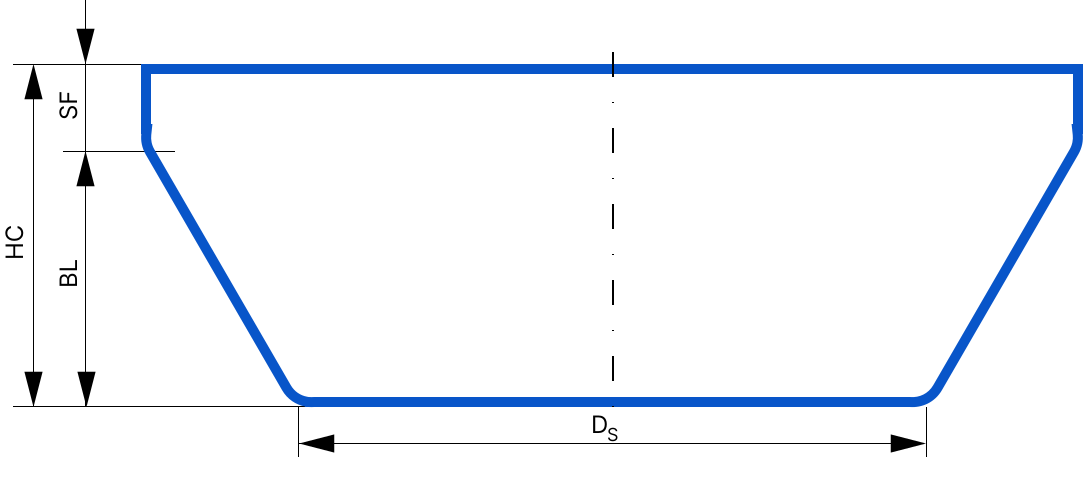
Separate formula based on the outside diameter: CR = 0.8×Do

DIN 28013 semi-ellipsoidal head

The German standard common in European process vessels

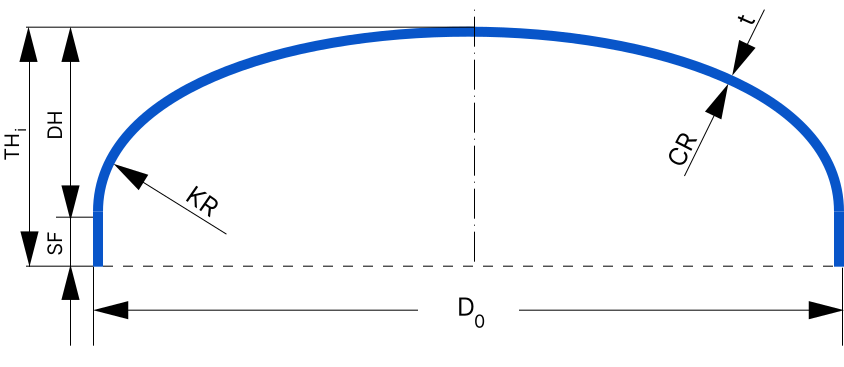
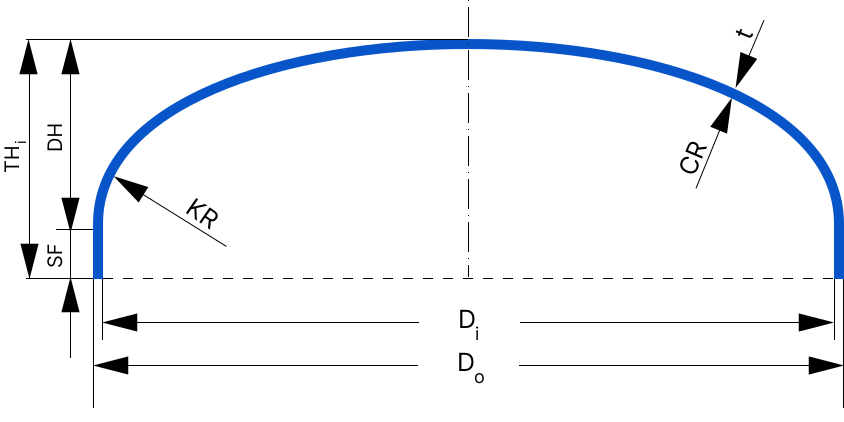
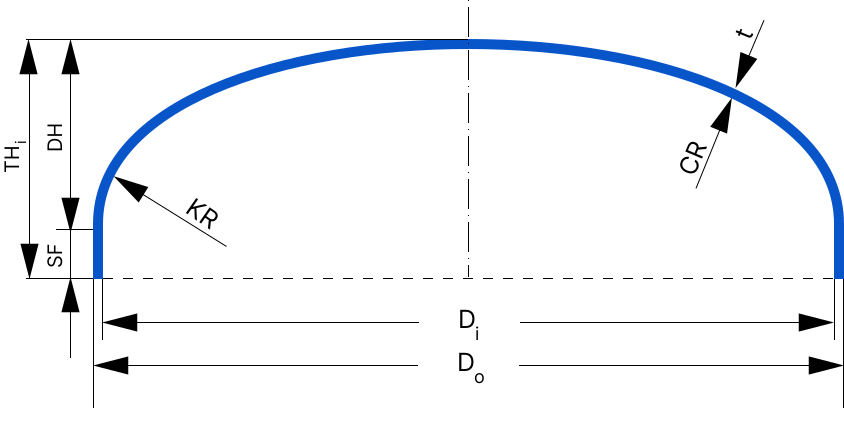
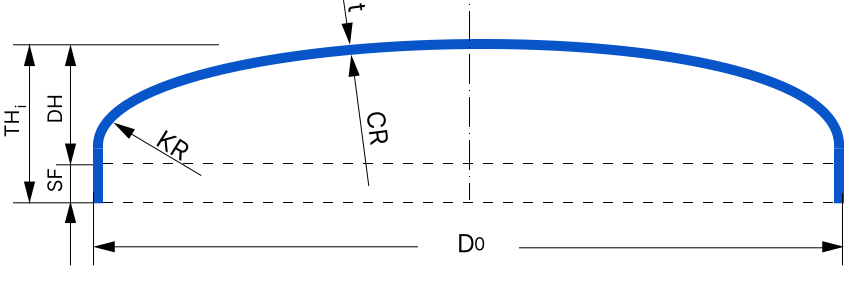
The semi-ellipsoidal head to the German standard DIN 28013 is defined by two parameters: crown radius CR = 0.8×Do and knuckle radius KR = 0.154×Do (both based on the vessel's outside diameter). These ratios were chosen to create a shape between torispherical and 2:1 elliptical.
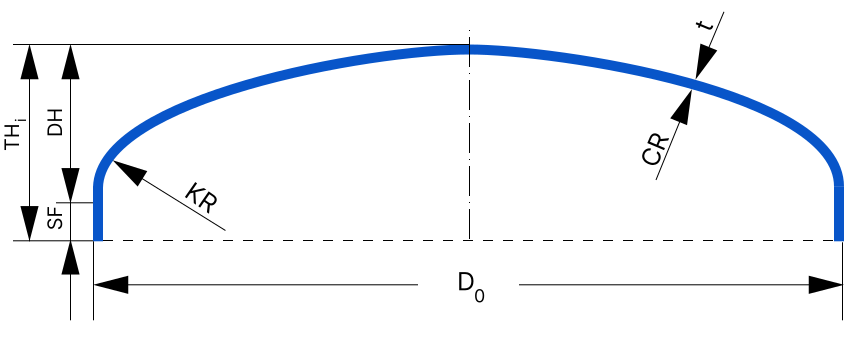
Semi-ellipsoidal DIN 28013

Semi-ellipsoidal DIN 28013

  • CR = 0.8 × Do
  • KR = 0.154 × Do
  • SF ≥ 3 × t
  • DH = 0.255×Do − 0.635×t
  • THi = SF + DH
  • DH 355 mm
  • THi 397 mm
  • KR 218 mm
  • CR 1133 mm
  • SF 42 mm
CR formula
CR = 0.8 × Do
KR formula
KR = 0.154 × Do
SF formula
Greater of 3×t or 0.03×Di
Reference standard
DIN 28013 (Germany)
Separate formula based on the outside diameter
Larger knuckle radius than torispherical
A shape between torispherical and 2:1 elliptical
Common in European process equipment
More even stress and less thickness
Plate material certificate with every shipment

What is a DIN 28013 semi-ellipsoidal head?

The semi-ellipsoidal head to the German standard DIN 28013 is defined by two parameters: crown radius CR = 0.8×Do and knuckle radius KR = 0.154×Do. These ratios create a shape between torispherical and 2:1 elliptical.

This standard is particularly common in the process industries of Germany and Central Europe. Its SF is taken as at least 3 times the plate thickness, slightly less than the 3.5 times common in other standards.

Geometry formulas of the DIN 28013 head

Both main parameters are defined from the vessel's outside diameter:

Crown radius
CR = 0.8 × Do
Knuckle radius
KR = 0.154 × Do
Dish height
h ≈ 0.255 Do
Straight flange
SF ≥ max(3 t, 0.03 Di)
Workshop note

Unlike many heads that define CR/KR from Di, DIN 28013 takes both from Do; keep this difference of basis in mind when matching it to ASME projects.

Online calculation

See the head's dimensions, volume and weight for a real diameter and thickness

DIN 28013 semi-ellipsoidal head

Semi-ellipsoidal DIN 28013

Semi-ellipsoidal DIN 28013

  • CR = 0.8 × Do
  • KR = 0.154 × Do
  • SF ≥ 3 × t
  • DH = 0.255×Do − 0.635×t
  • THi = SF + DH
  • DH 355 mm
  • THi 397 mm
  • KR 218 mm
  • CR 1133 mm
  • SF 42 mm

Liquid level and volume inside this head

How the head is mounted
Internal surface area of the head0m²
Plate weight of this head0kg
Liquid weight at this level0kg
Full capacity of this head0m³
Liquid volume in this head0m³
Total weight (fluid + head)0kg

Development of this head (flat blank before forming)

The diameter of a flat plate of the same thickness and material that weighs the same as the formed head — an initial workshop estimate based on equal weight, not allowing for thickening or extra stretching at the knuckle.

Flat blank radius (development)0mm
Flat blank diameter (development)0mm
Flat blank area0m²

The vessel head production process

From calculating the blank diameter to final edge preparation — the steps of making a vessel head in the workshop

  1. Calculating the blank diameter

    Cutting a disc from plate with the diameter and thickness calculated for the head type and vessel diameter

  2. Cutting the plate blank

    Precise cutting of steel or stainless plate by plasma, laser or gas according to the technical drawing

  3. Pressing the head

    Hot or cold forming of the disc with a die and industrial press until it reaches the final head profile

  4. Edge preparation

    Machining the edge, bevelling and preparing the weld area for fitting to the vessel shell
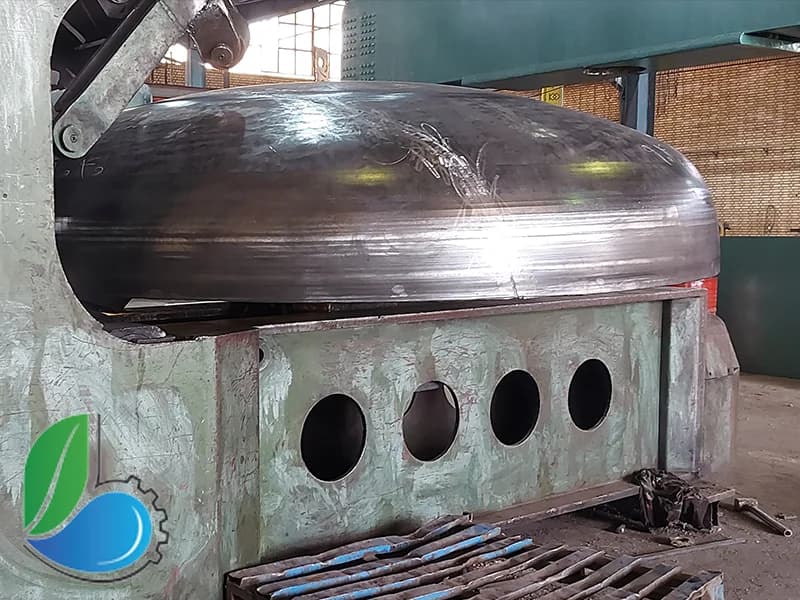
Pressing a vessel head in the Behineh Ab workshopVideo coming soon

Choosing a head: the balance between pressure, cost and time

If the client or project standard explicitly requires DIN, or similar earlier equipment in the production line was built to this standard, staying with DIN 28013 makes it simpler to keep the technical documentation consistent.
1Take the design pressure and temperature from the data sheet
2Check the height limit at the installation site
3Compare the cost of plate with the cost of pressing
4Consider die availability and delivery time
Pressed heads in the workshop store

Applications and industries served

Process vessels in the pharmaceutical and biotechnology industries
Food industry equipment to the German standard
Chemical vessels with a DIN design basis
Export projects for the German and Central European market

Buying heads from Behineh Ab

Six steps from first contact to delivery

1Send the head specifications

Give the outside diameter, plate thickness, head type and required material.

2Technical quotation

The calculated weight, unit price and delivery time are sent the same business day.

3Plate supply

Plate is supplied with the mill certificate and inspected on arrival before cutting.

4Cutting and pressing

Cutting the disc, hot or cold pressing depending on thickness, and checking dimensions with a template.

5Edge machining and bevelling

Machining the cylindrical edge and bevelling it ready for welding to the shell.

6Packing and shipping

Packing, issuing the part identification sheet and shipping nationwide.

What sets us apart

Ready dies for the most common diameters
Thickness checked after pressing with a thickness gauge
Profile checked against a reference template for each form
Plate material certificate with every shipment
Hot pressing for thicknesses above 16 mm
Stainless and galvanized heads available

Price inquiry
vessel head

Enter the diameter, thickness and head type; you will receive the calculated weight and unit price.

  • Quotation with the exact weight of the part
  • Standard heads delivered in 7 business days
  • Shipping nationwide
Direct line to engineering office
021 - 3345 6789

Your information is confidential and used only to prepare a technical proposal.

Other head types

All articles
  • Assembling the shell and head of a steel tank in the Behineh Ab tank fabrication workshop

    Steel Tank Manufacturing Steps, from Order to Delivery

    The steps of building a steel tank, from the data sheet to testing and dispatch. A 20,000-litre tank takes about three weeks; here is what that time is spent on.

    Read more
  • Inspector carrying out a non-destructive test on a steel tank shell weld

    Tank Tests: What Defect Does Each Test Find?

    Hydrotest, radiography, ultrasonic, liquid penetrant, magnetic particle and vacuum box. Each finds a particular defect and none can replace another. Here we compare them.

    Read more
  • Pressure vessel under hydrostatic test with a pressure gauge in the Behineh Ab workshop

    Tank Hydrostatic Test, Step by Step

    The hydrotest is a tank's final exam before delivery, and we carry it out in our own factory. The test pressure, the work before filling, and the mistake that can ruin a tank while it is being drained.

    Read more
  • Radiography film of a tank shell weld on a film viewer

    Weld Radiography: What Percentage of Seams Must Be Tested?

    The radiography percentage sets the joint efficiency, and the joint efficiency sets the plate thickness. In other words, this decision directly affects the tank's weight and price.

    Read more