How weld thickness and material grade drive the need for heat treatment.
Code criteria for PWHT
Fabrication codes use weld thickness and steel grade to decide when PWHT is mandatory. Skipping it can lead to delayed cracking and rejection at final inspection.
A common thickness threshold
| Material group | Common thickness threshold | Requirement |
|---|---|---|
| Ordinary carbon steel (P-1) | Typically around 32 mm and up | PWHT becomes mandatory |
| Low-alloy steel | Lower threshold than carbon steel | Check against the grade and governing code |
| Austenitic stainless steel | Usually no PWHT needed | Sensitization risk should be assessed separately |
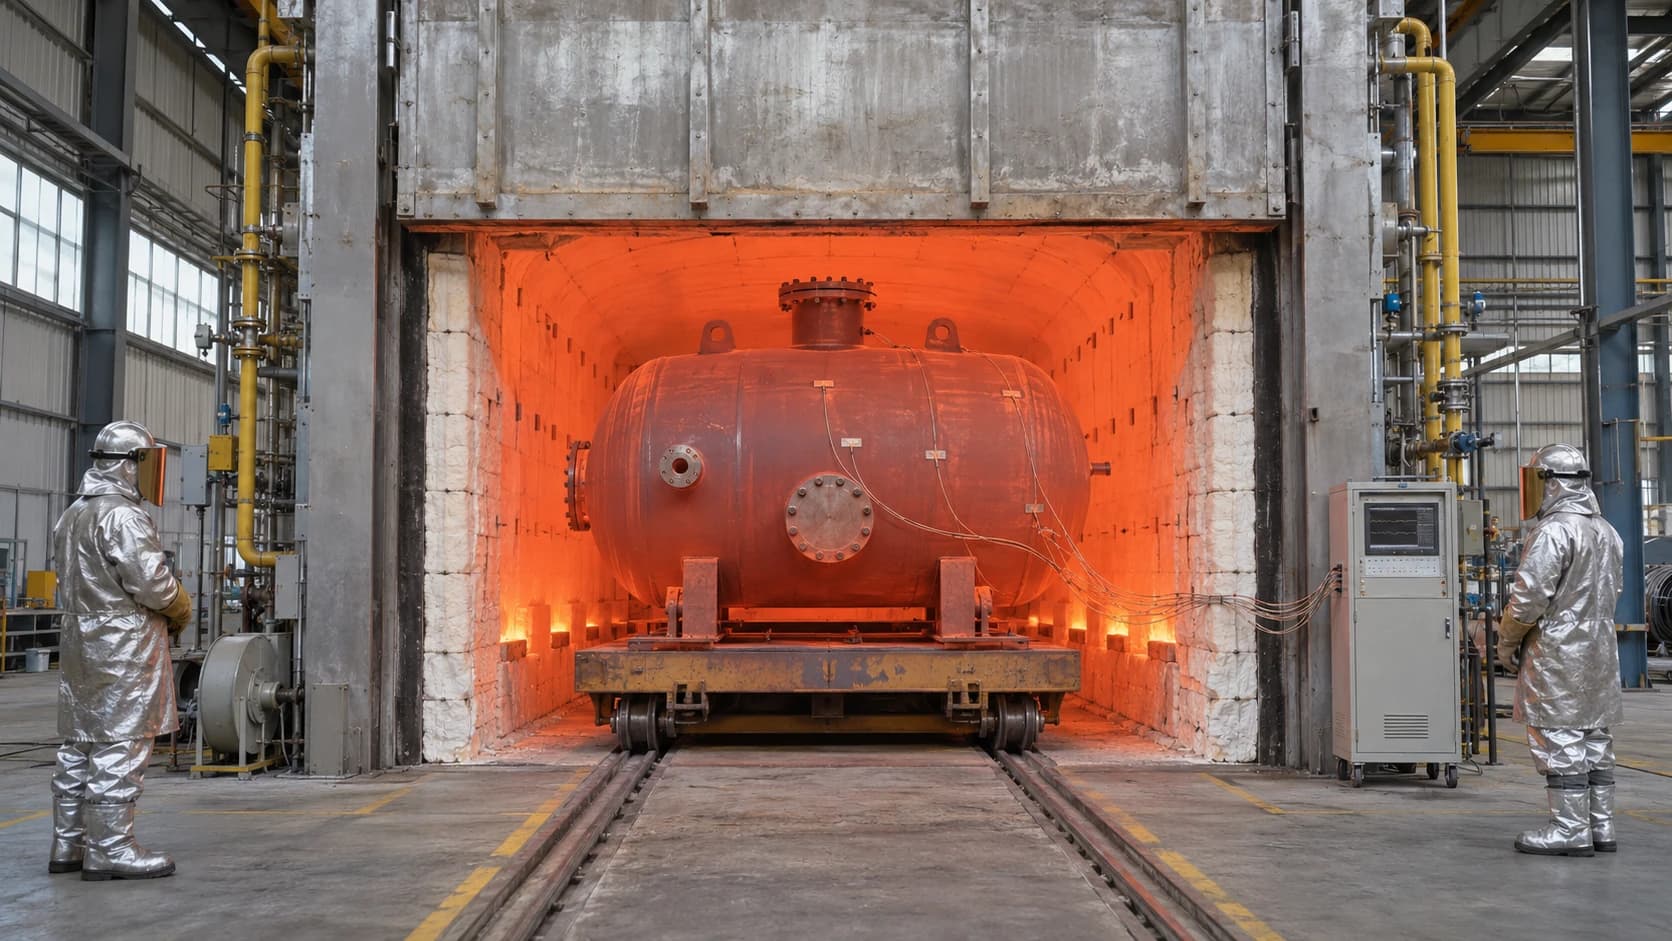
PWHT can be done in a furnace for the whole vessel, or locally around a single joint. Local PWHT suits repairs or field joints that can't be moved to a furnace, but demands tighter control of the temperature gradient.